A batching plant rarely fails without warning. A slipping conveyor belt, unstable moisture sensor, or blocked cement screw can quietly reduce concrete quality before production stops. This is why “How to troubleshoot batching plant malfunctions” must begin with observation, not guesswork.
Concrete technology educator Dr. Ken Hover has emphasized a practical principle: “Concrete quality begins with control, not correction.” That idea fits every plant control room. Operators should compare the control panel readings with physical conditions. Is the aggregate actually moving? Is the mixer discharge gate fully opening? Does the weigh hopper return to zero after each batch? Small discrepancies matter.
Safety comes first. Stop the equipment before inspecting moving parts, electrical cabinets, or pressurized lines. Check alarms, sensor cables, air pressure, and material buildup in a fixed sequence. Record the fault code and the exact time it appeared. A wet aggregate pile can explain a slump change better than a damaged mixer. Sometimes, the obvious cause is wrong.
The troubleshooting process should also examine maintenance history. A plant may appear mechanically sound while its calibration has slowly drifted. Test load cells with approved procedures, inspect worn mixer arms, and verify moisture probes against representative samples. Do not replace expensive components too quickly. The first diagnosis may be incomplete. Reliable results come from evidence, repeatable checks, and experienced judgment. This approach protects workers, reduces wasted batches, and helps maintain consistent concrete production under demanding conditions.
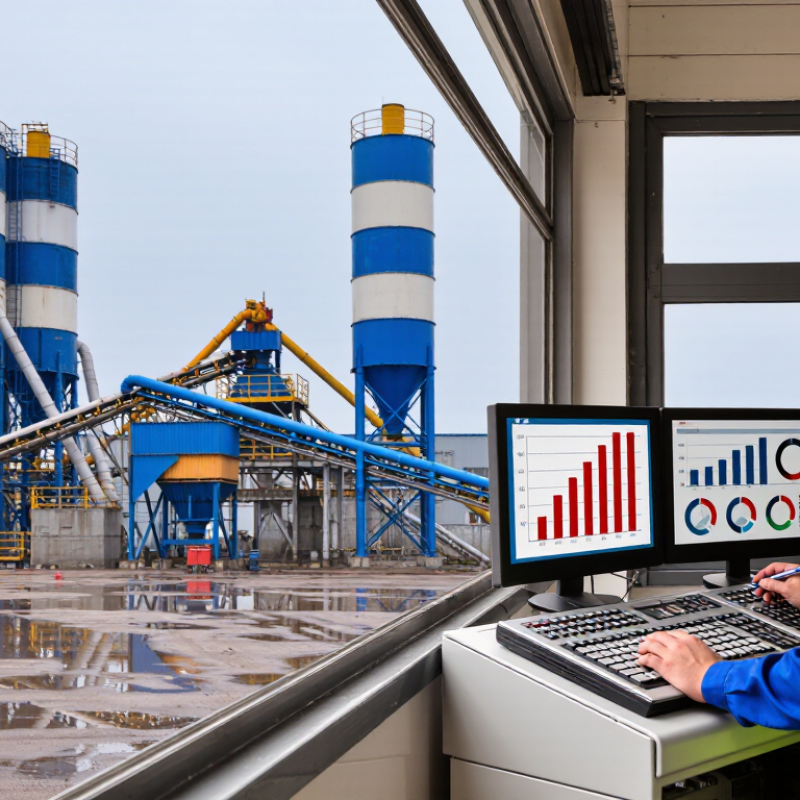
Reliable troubleshooting starts with recognizing warning signs before production stops. Uneven aggregate moisture can cause sudden slump changes and inaccurate water dosing. Watch for damp material clinging to the bin walls. A conveyor that jerks, slips, or produces rubber dust may have poor tension or misalignment. These signs deserve attention.
Mixer problems often appear as unusual vibration, metallic noise, or longer discharge times. Check the blades, shaft, and trapped hardened concrete after isolating power safely. A drifting load cell may show unstable readings when the hopper is empty. Compare the zero value with previous maintenance records. Do not trust one display reading alone. Physical checks matter.
Dust around the filter can indicate damaged seals, blocked cartridges, or excessive pressure. A cement screw that starts slowly may have moisture buildup or worn bearings. Inspect cables for heat marks and loose terminals, especially after heavy rain. I have seen teams replace sensors when a simple mechanical blockage caused the alarm. That mistake wastes time. Record each symptom, batch number, temperature, and inspection result. Small details often reveal repeating faults. Stop operation when guards, emergency devices, or structural parts appear damaged. Never bypass an alarm to maintain output.
| No. | System or Component | Common Malfunction | Warning Signs | Likely Causes | Recommended Checks | Corrective Action | Priority |
|---|---|---|---|---|---|---|---|
| 1 | Aggregate Bins and Gates | Aggregate discharge is slow, incomplete, or blocked. | Irregular material flow, unusual vibration, or an empty-bin alarm while material remains in the bin. | Moist or oversized aggregate, material bridging, worn gate seals, or insufficient gate-cylinder pressure. | Inspect aggregate moisture and particle size; check the gate opening, cylinder movement, air pressure, and buildup around the outlet. | Remove the blockage safely, clean buildup, restore the specified air pressure, and replace damaged seals or pneumatic components. | High |
| 2 | Aggregate Weighing System | Aggregate weights do not match the programmed values. | Frequent weighing corrections, unstable readings, or noticeable differences between batches. | Load-cell damage, mechanical contact, material accumulation, poor calibration, or an unstable foundation. | Confirm that the weighing hopper is freely suspended; inspect load-cell cables, mounting points, zero reading, and calibration records. | Remove foreign material, correct mechanical interference, secure connections, and recalibrate the weighing system using certified test weights. | High |
| 3 | Cement, Fly Ash, or Mineral Powder Silo | Powder does not flow consistently from the silo. | Low discharge rate, silo pressure changes, arching, or repeated high-level and low-level alarm errors. | Moisture intrusion, powder compaction, blocked aeration pads, faulty venting, or an overfilled silo. | Check silo filters, pressure-relief devices, aeration equipment, material moisture, and the condition of the discharge cone. | Clean or replace filters, restore aeration, remove compacted material according to the safety procedure, and prevent moisture entry. | High |
| 4 | Screw Conveyor | Powder transfer is slow, stops, or produces abnormal noise. | Motor overload, high current, rattling, vibration, or powder leakage at the shaft seal. | Foreign material, excessive powder buildup, worn bearings, damaged flighting, misalignment, or inadequate lubrication. | Isolate power and inspect the conveyor housing, inlet, outlet, bearings, couplings, shaft alignment, and motor current. | Clear the obstruction, replace worn bearings or seals, correct alignment, lubricate as specified, and verify the motor load. | High |
| 5 | Water Dosing System | Water quantity is inaccurate or dosing is interrupted. | Unstable flow, delayed valve response, leaking pipes, or concrete slump changes between batches. | Blocked filter, faulty flow meter, valve wear, pump cavitation, low supply pressure, or incorrect calibration. | Inspect the water source, filter, pump, valves, flow meter, pipework, and actual volume delivered during a test cycle. | Clean the filter, remove air from the line, repair leaks, service the pump or valve, and recalibrate the flow-measuring device. | Medium |
| 6 | Admixture Dosing System | Admixture dosage is inconsistent or the pump fails to prime. | Foaming, air bubbles, crystallization, low tank level, or concrete workability outside the target range. | Incorrect admixture concentration, clogged suction line, incompatible storage conditions, worn pump parts, or an empty tank. | Check the tank level, concentration, suction hose, strainer, pump seals, calibration container, and storage temperature. | Use the specified admixture concentration, clean the suction system, replace worn parts, remove trapped air, and recalibrate the pump. | Medium |
| 7 | Mixing Unit | Concrete is not mixed uniformly or the mixing cycle is unusually long. | Visible dry pockets, inconsistent slump, excessive noise, high motor current, or material accumulation on the mixer walls. | Worn mixing paddles, incorrect clearance, overloading, insufficient mixing time, poor charging sequence, or hardened concrete buildup. | Inspect paddles, liners, discharge doors, mixer clearance, motor current, batch size, and the programmed mixing time. | Remove hardened buildup, adjust or replace worn wear parts, correct the charging sequence, and set the proper batch size and mixing time. | High |
| 8 | Mixer Discharge Door | Discharge door does not open fully or does not close tightly. | Concrete leakage, slow discharge, door-position alarm, or hydraulic and pneumatic pressure fluctuations. | Hardened concrete around the door, damaged seals, bent linkage, faulty actuator, or low operating pressure. | Inspect the door path, seals, hinges, linkage, actuator, limit switches, and pressure supply after isolating the equipment. | Clean the door area, adjust linkage, replace seals or the actuator when necessary, and verify open and closed position signals. | High |
| 9 | Compressed-Air System | Pneumatic cylinders operate slowly or fail to move. | Frequent compressor cycling, audible air leakage, low pressure, water in the air line, or sluggish gate movement. | Air leaks, clogged filters, excessive condensate, inadequate compressor capacity, damaged seals, or incorrect regulator settings. | Read the pressure gauge, inspect hoses and fittings, drain the receiver, check the filter-regulator-lubricator unit, and test for leaks. | Repair leaks, drain condensate, clean or replace filters, adjust pressure within the specified range, and service cylinder seals. | High |
| 10 | Electrical Control Panel | Equipment stops unexpectedly or cannot start. | Circuit-breaker trips, fault codes, overheated components, control voltage loss, or intermittent communication. | Overload, short circuit, loose terminals, damaged cable, phase loss, overheating, or an active safety interlock. | Review alarms and event logs; check supply voltage, phase balance, terminals, fuses, overload settings, and safety circuits. | Keep the system isolated during inspection, tighten or replace defective electrical parts, reset only after the cause is corrected, and test all interlocks. | High |
| 11 | Control Software and Sensors | Incorrect sequence, missing signal, or communication failure occurs. | Sensor status remains unchanged, duplicated readings, delayed commands, or repeated controller communication alarms. | Sensor misalignment, damaged wiring, network interruption, incorrect configuration, or moisture and dust contamination. | Compare sensor status with the physical position; inspect connectors, input/output signals, network cables, and configuration parameters. | Clean and align sensors, repair wiring, restore approved settings, replace failed sensors, and perform a controlled sequence test. | Medium |
| 12 | Dust Collector and Ventilation | Dust escapes from the mixer or silo during loading. | Visible dust cloud, rising filter differential pressure, reduced suction, or frequent filter-cleaning cycles. | Blocked or damaged filter elements, faulty pulse-cleaning valves, poor duct sealing, or insufficient fan performance. | Check differential pressure, filter condition, pulse-air pressure, cleaning valves, duct joints, and fan rotation. | Replace damaged filters, repair leaks, service the pulse-cleaning system, and confirm adequate airflow before resuming normal production. | High |
| 13 | Conveyor or Skip Hoist | Aggregate transfer is interrupted or the skip moves unevenly. | Belt drift, slipping, abnormal vibration, brake noise, overload trips, or delayed upper and lower limit signals. | Misaligned belt, worn pulley or cable, overloading, inadequate tension, brake wear, or faulty limit switch. | Inspect belt or cable alignment, tension, pulleys, brakes, limit switches, guards, and motor current. | Remove spillage, align and tension the conveyor, replace worn components, adjust brakes, and test limit protection before operation. | High |
| 14 | Lubrication and Mechanical Drives | Bearings or drive components overheat and wear prematurely. | High temperature, grease leakage, metallic noise, vibration, or visible shaft movement. | Insufficient or excessive lubrication, contamination, misalignment, worn bearings, or excessive belt or chain tension. | Measure temperature and vibration; inspect lubricant condition, bearing play, shaft alignment, and drive tension. | Lubricate with the specified product and quantity, correct alignment and tension, and replace damaged bearings or drive parts. | Medium |
| 15 | Calibration and Quality Control | Batch proportions are correct on screen but concrete quality varies. | Variable slump, inconsistent strength results, changing aggregate moisture, or frequent operator adjustments. | Uncompensated aggregate moisture, scale drift, incorrect material settings, poor sampling, or inconsistent mixing conditions. | Verify moisture content, scale calibration, material density, recipe settings, sample method, and mixing time. | Update moisture compensation, recalibrate scales, verify material parameters, standardize sampling, and document corrective results. | High |
Stop safely and record the alarm, batch number, material moisture, and exact time. Do not reset everything immediately. These details can reveal repeated patterns.
Inspect the electrical cabinet for loose terminals, burnt insulation, blown fuses, and moisture. Measure incoming voltage with qualified equipment. Check motor overloads and sensor power supplies.
Listen for gearbox noise, belt slipping, unusual vibration, or blocked discharge gates. Inspect bearings, mixer paddles, and hardened material near the outlet. Small buildup can increase the load sharply.
Look for oil leaks, low reservoir levels, cracked hoses, and slow cylinder movement. Check pressure readings carefully. Warm oil may indicate internal leakage or a restricted filter.
Compare displayed signals with actual component positions. Review input and output status before replacing parts. A drifting load cell, dirty proximity sensor, or loose communication cable can create false faults.
Press each emergency-stop button and confirm immediate shutdown. Check guard switches, access-door interlocks, overload protection, and alarm lights. Never bypass an interlock.
Compare load-cell readings with a certified test weight. Check moisture sensors against a recent material sample. Clean dust and water from sensor faces, connectors, and wiring.
Run the sequence without material. Confirm that gates open in order, conveyors start correctly, and mixer timing signals arrive properly. A normal-looking sequence can still produce uneven batches.
Ask for help when faults repeat, readings remain unstable, or panels require opening. Use lockout procedures before maintenance. Record every test, including normal readings. One overlooked detail may be grounding. Recheck it.
This guide explains How to troubleshoot batching plant malfunctions by identifying common warning signs before they develop into serious failures. It covers how to inspect electrical circuits, mechanical components, hydraulic systems, and control units to locate the source of abnormal noise, inaccurate weighing, slow operation, or unexpected shutdowns. It also addresses material feeding, mixing, and discharge problems, including blockages, uneven batching, and inconsistent output.
The guide further describes how to test safety devices, sensors, and automated control functions to confirm that the plant operates reliably and safely. After finding the cause, operators can apply suitable repairs, clean and adjust affected components, and verify system performance through controlled testing. Preventive maintenance, regular inspections, accurate calibration, and proper restart procedures are also emphasized to reduce downtime, improve product consistency, and support stable long-term operation.
 Cloverdyn Plant