Mobile concrete plants bring batching closer to demanding construction sites, but proximity does not guarantee reliable production. Limited space, uneven ground, changing weather, and frequent relocation can expose weak systems quickly. A small moisture error in sand may alter slump, strength, and cement consumption across several truckloads. That is why contractors should ask: What are common issues in mobile concrete plants?
Industry guidance supports a disciplined approach. ACI 304.6R, Guide for Use of Volumetric-Measuring and Continuous-Mixing Concrete Equipment, emphasizes accurate proportioning, material control, and equipment inspection. The National Ready Mixed Concrete Association also stresses calibration, mixer performance, storage management, and quality documentation in its plant certification resources. These details matter when aggregate bins sit beside muddy access roads or when a water tank loses pressure during peak production. The problem is rarely one dramatic failure. It is usually a chain of small oversights.
Safety and environmental performance also deserve attention. OSHA’s respirable crystalline silica standard sets a 50 micrograms per cubic meter, eight-hour permissible exposure limit for covered workplaces. Dust control, enclosed transfer points, and effective housekeeping are therefore operational priorities. The Global Cement and Concrete Association reports that concrete contributes roughly 7% of global carbon dioxide emissions, making material waste and unnecessary cement use important concerns. This guide examines ten common issues, including inconsistent batching, blocked conveyors, poor washout control, power interruptions, and delayed maintenance. Some conclusions may differ by plant design and climate. Field records, calibration logs, and operator experience should challenge every assumption.
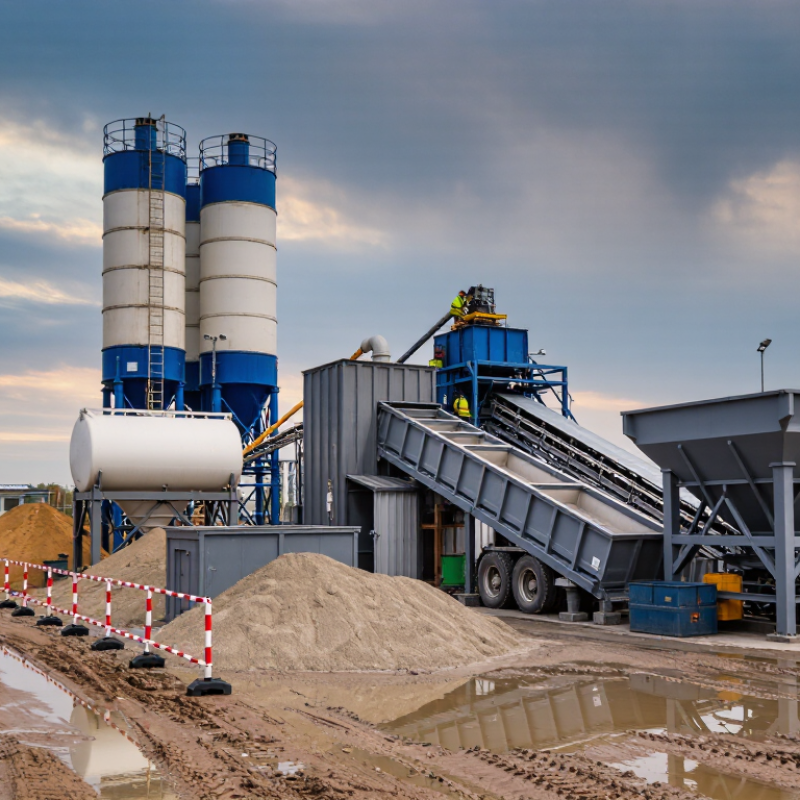
In mobile concrete plants, aggregate feeding problems often begin in the storage area. During site inspections, I have seen mixed sizes placed in one pile. This quickly changes the intended mix ratio. Keep coarse and fine aggregates in separate, clearly marked bays. Use firm, level ground beneath each pile. Poor drainage can turn the lower material into wet, contaminated mass. Moisture matters.
A loader may deliver material unevenly when the stockpile face is too steep. Feeding hoppers can then receive sudden surges or empty pockets. Bridging is common when damp sand sticks to hopper walls. Operators should check hopper outlets, gates, and vibration devices before each shift. Do not rely only on automatic controls. Watch the actual flow. A short manual check can reveal a slow belt or a blocked opening.
Accurate feeding also depends on clean weighing equipment. Remove buildup from load cells, belts, and scraper edges. Verify belt scale readings with known test loads at regular intervals. Rain can raise aggregate moisture within hours, so moisture readings should guide water adjustments. Record these changes beside production data. The process is not perfect. A rushed crew may skip a check, especially during a busy pour. Small errors accumulate. Clear stockpile labels, stable loading habits, and frequent inspections reduce that risk.
Cement, water, and admixture dosing inaccuracies are common problems in mobile concrete plants. They can reduce strength, change slump, and create uneven batches. A small cement error may seem harmless, but repeated errors quickly affect project quality.
Moisture inside sand is a frequent cause of water imbalance. After rain, the same loader bucket may contain much more water than expected. Operators should check aggregate moisture regularly and adjust the batch water accordingly. Load cells also need inspection, especially after relocation. Dust, vibration, and uneven ground can distort readings. Keep the plant level. It matters.
Water meters require practical verification, not blind trust. A measured container can reveal flow errors within minutes. Admixture lines deserve similar attention. Dried residue may narrow the hose and delay chemical delivery. Flush the line according to the equipment procedure, then compare the measured output with the control setting. Simple checks work. Sometimes.
Accurate records support reliable decisions. Note the batch number, material weights, moisture readings, and observed slump. When results drift, compare the records before changing the mix design. Experienced technicians also check whether a valve closed fully or a pump pulsed unexpectedly. Our checks are not flawless. Human entry errors still occur, particularly during busy pours. A second person should review unusual readings before production continues. Independent scale calibration and routine maintenance provide stronger evidence than assumptions.
Mobile concrete plants often produce inconsistent concrete because small process changes become large quality variations.
A damp aggregate pile can add unexpected water. A worn mixer blade can leave dry pockets. Field crews may also shorten mixing time when traffic builds. That shortcut is costly.
ASTM C94/C94M allows only a 25 mm slump tolerance when the specified slump is 100 mm or less. A 40 mm error can therefore signal poor water control, not harmless variation.
Operators should record aggregate moisture before batching and verify the scale readings every shift. The National Ready Mixed Concrete Association recommends documented quality-control checks, yet many mobile teams still rely on visual judgment. We do too often.
ACI 214R-11 links concrete uniformity with statistical variation.
Its guidance treats a coefficient of variation below 10% as excellent, while variation above 20% demands attention.
Track compressive-strength results, slump, air content, batch time, and water additions together. ACI 318-19 also evaluates strength through consecutive test results, not one impressive cylinder. That matters.
A strong sample can hide a weak load. We sometimes trust the gauge too much.
A simple mistake remains possible: the moisture probe may be clean, but incorrectly calibrated. Review the records, inspect the mixer, and question results that look unusually perfect.
Transport, setup, and on-site operation create many mobile concrete plant problems. Narrow access roads can delay delivery, while soft ground may destabilize support legs. A 15-minute delay can disturb the entire pour sequence. According to the U.S. Environmental Protection Agency, a heavy-duty diesel truck may burn about 0.8 gallons per hour while idling. Poor scheduling therefore increases fuel use and site congestion.
Setup needs more than a level surface. Crews must check ground bearing capacity, water access, electrical supply, aggregate stockpile distance, and mixer clearance. Incorrect calibration can produce inconsistent slump or cement content. The NRMCA Concrete Plant Operations Manual stresses regular inspection, moisture correction, and scale verification. These details are often rushed. That assumption is weak. Uneven aggregate moisture can change batch performance faster than operators expect.
On-site operation also depends heavily on skilled people. The Associated General Contractors of America’s 2024 Workforce Survey reported that 94% of respondents struggled to fill salaried positions, while 92% faced difficulty finding craft workers. Less experienced crews may miss buildup around gates, blocked discharge chutes, or delayed washout. Dust control requires attention too. OSHA’s respirable crystalline silica standard sets a permissible exposure limit of 50 micrograms per cubic meter over eight hours. A practical improvement is simple: assign one person to monitor production, traffic, and housekeeping continuously. Even then, the plan may need revision when weather changes.
| No. | Common Issue | Main Phase | Typical Frequency | Typical Delay | Primary Causes | Operational Impact | Recommended Controls |
|---|---|---|---|---|---|---|---|
| 1 | Route Restrictions and Transport Delays | Transport | High | 2–8 hours | Low bridges, narrow roads, axle-weight limits, traffic restrictions, permit requirements, and unsuitable access roads. | Schedule slippage and additional haulage cost | Complete a route survey, verify legal dimensions and axle loads, obtain permits early, and prepare an alternative route. |
| 2 | Unstable or Poorly Prepared Site Ground | Setup | High | 4–24 hours | Soft soil, inadequate compaction, standing water, insufficient working space, or lack of a level foundation. | Unsafe setup and inaccurate weighing | Inspect and compact the platform, provide drainage, confirm level tolerances, and use suitable support plates or foundations. |
| 3 | Limited Water, Power, or Utility Connections | Setup / Operation | Medium | 1–6 hours | Insufficient water flow, unstable electrical supply, inadequate generator capacity, or long temporary cable runs. | Startup interruptions and reduced output | Calculate peak demand, test connections before production, install protection devices, and maintain backup water and power capacity. |
| 4 | Aggregate Moisture and Gradation Variation | Material Handling / Batching | High | 15–60 minutes | Rainfall, inconsistent stockpiles, segregation, wet sand, and changes in aggregate supply. | Slump variation and water-cement ratio errors | Measure moisture regularly, adjust batch water, maintain separate stockpiles, and use first-in, first-out material control. |
| 5 | Incorrect Calibration of Weighing Systems | Setup / Quality Control | Medium | 1–4 hours | Load-cell movement, material buildup, zero drift, uneven supports, or calibration not verified after relocation. | Out-of-tolerance concrete batches | Perform zero checks and test-weight verification after setup, keep weigh hoppers clear, and document calibration results. |
| 6 | Material Bridging, Blockages, and Spillage | On-Site Operation | High | 15–90 minutes | Wet or cohesive aggregate, oversized particles, cement buildup, restricted chutes, and poorly managed stockpiles. | Interrupted batching and cleanup labor | Control material moisture, inspect transfer points, clean safely at planned intervals, and never clear blockages while equipment is energized. |
| 7 | Cement Silo Flow Problems and Dust Release | Material Handling | Medium | 30–120 minutes | Moisture ingress, silo rat-holing, overfilled filters, faulty aeration, or excessive filling pressure. | Cement feed interruption and environmental nonconformance | Keep cement dry, inspect filter units and pressure-relief devices, monitor silo levels, and use dust-control procedures during filling. |
| 8 | Weather-Related Concrete Temperature and Slump Changes | Production / Delivery | High | 15–60 minutes | High ambient temperature, cold weather, wind, evaporation, hot aggregates, or delayed placement. | Reduced workability and accelerated or delayed setting | Monitor concrete temperature, protect stockpiles, coordinate delivery timing, and follow the approved mix-design and admixture procedure. |
| 9 | Washout, Runoff, and Waste Management | On-Site Operation / Compliance | Medium | 30 minutes–4 hours | No designated washout area, inadequate containment, poor drainage, and uncontrolled concrete residue. | Cleanup cost and potential regulatory action | Install lined containment, separate alkaline wash water from stormwater, inspect discharge points, and maintain waste records. |
| 10 | Maintenance, Spare Parts, and Operator Coordination Gaps | On-Site Operation | High | 1–8 hours | Remote sites, limited technicians, delayed parts, unclear responsibilities, insufficient inspections, and poor communication with truck drivers. | Unplanned downtime and missed pours | Use a preventive-maintenance checklist, stock critical consumables, assign clear roles, conduct toolbox meetings, and maintain a daily production log. |
Mobile concrete plants face ten recurring problems: aggregate moisture errors, belt misalignment, mixer wear, clogged filters, inaccurate water meters, failed sensors, PLC interruptions, poor guarding, silica dust, and uncontrolled washout water. These issues often appear during rushed setup. A conveyor may track correctly in the morning, then spill material after a wet delivery. Small errors can change slump, increase cement use, and create rejected loads.
Maintenance records should include lubrication, bolt torque, belt tracking, calibration, and emergency-stop tests. Automation improves consistency, but a failed moisture probe can quietly produce incorrect water-cement ratios. Manual checks still matter.
OSHA limits respirable crystalline silica exposure to 50 micrograms per cubic meter over an eight-hour shift. Dust control therefore needs enclosed transfer points, local extraction, housekeeping, and suitable respiratory protection. The U.S. EPA’s AP-42 guidance identifies material handling and traffic as important particulate emission sources. Water sprays alone may hide a problem rather than solve it.
Tips: Inspect the plant before each relocation. Lock out energy sources before clearing a jam. Keep washout contained, because alkaline runoff can damage soil and waterways.
The Global Cement and Concrete Association reports that cement production contributes about 7% of global carbon dioxide emissions, so reducing rejected batches has environmental value.
BLS recorded 1,069 construction fatalities in the United States in 2022. That figure is sobering, although concrete plants are not the only cause. Review near misses, not just injuries.
A checklist can fail when nobody challenges its assumptions.
Store coarse and fine aggregates in separate, clearly marked bays. Use firm, level ground with good drainage. Wet lower material can become contaminated. Moisture matters.
A steep stockpile face can cause sudden surges or empty pockets. Loaders should feed steadily and avoid uneven bucket deliveries. Watch the flow directly. Automatic controls can miss problems.
Inspect hopper outlets, gates, and vibration devices before every shift. Damp sand may stick to hopper walls. A short manual check helps reveal blocked openings.
Rain can increase sand moisture within hours. Operators should measure moisture and adjust batch water accordingly. The same bucket may carry much more water after rain.
Remove buildup from load cells, belts, and scraper edges. Verify belt scales with known test loads regularly. Keep the plant level. Readings can drift.
Check water meters with a measured container. Inspect hoses for dried residue and restricted flow. Flush lines according to equipment procedures, then compare output with settings.
Record batch numbers, material weights, moisture readings, and observed slump. Compare records before changing the mix design. A second person should review unusual readings. Human errors still happen.
Narrow roads may delay delivery, while soft ground can destabilize support legs. Check ground capacity, utilities, stockpile distance, and mixer clearance. A short delay can disturb the entire pour.
Assign one person to monitor production, traffic, and housekeeping continuously. Control dust and clean buildup around gates and discharge chutes. Weather may force changes. The original plan is not always enough.
Mobile concrete plants offer flexibility and fast deployment, but they can experience several operational challenges. What are common issues in mobile concrete plants? Typical problems include poor raw material storage, aggregate segregation, blocked feeding systems, and inconsistent material moisture. Inaccurate dosing of cement, water, or admixtures can also affect mix proportions, while worn components or unsuitable mixing times may lead to uneven concrete quality, reduced strength, or inconsistent workability.
Transport and setup can create additional difficulties, especially when the plant is installed on uneven ground or operated in limited space. On-site teams may also face challenges with calibration, automation controls, communication, and changing weather conditions. Regular maintenance is essential to prevent mechanical failures, excessive downtime, and unexpected repair costs. Finally, safe operating procedures, dust control, noise reduction, spill prevention, and proper staff training are important for maintaining efficient, reliable, and environmentally responsible production.
Cloverdyn Plant